
0102030405
Dry Type Transformer Manufacturer Evaluation: 10 Checks on Vacuum Casting, Windings and PD Test Bays
2026-08-21
Quick Answer (For EPC & Indoor Substation Procurement)
- A 10-check factory audit separates cast-resin dry type suppliers from cast-iron marketing — the 10 checks cover vacuum casting, windings, and PD test bay.
- The Tianan dry-type transformer manufacturing scope covers SC series and resin casting lines.
- The SC series 10kV dry-type transformer is the standard reference for procurement specification.
- Partial discharge (PD) test per IEC 60076-11 is the structural verification that the casting process executed correctly.
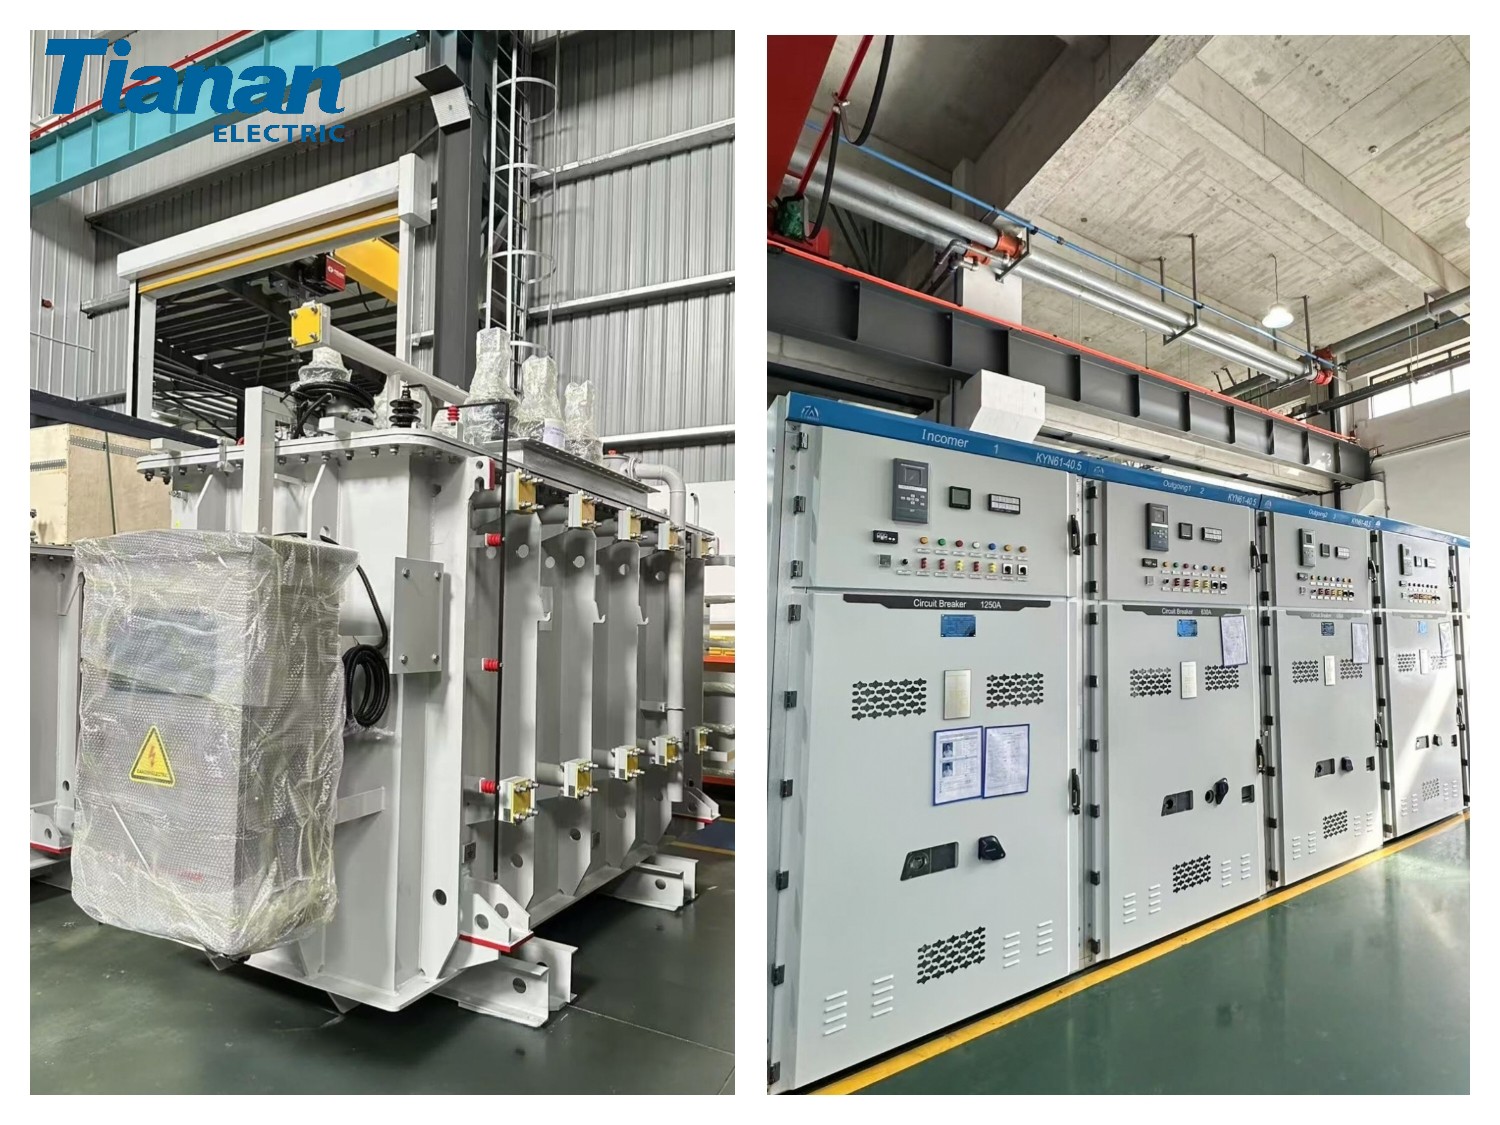
- The Tianan online factory tour documents the resin casting line and PD test bay.
Most EPC procurement teams evaluate Dry Type Transformer suppliers by reviewing catalog specifications and asking for type test reports.The result is a procurement pattern where the document review passes but the cast-resin quality issues surface only after the transformer is installed in the indoor substation, where partial discharge events trigger fire alarms or premature failure. The fix is to structure the supplier qualification as a 10-check factory audit that combines documentation review with physical verification of the vacuum casting, windings, and PD test bay.
The Tianan dry-type transformer manufacturing scope covers SC series and resin casting lines. The SC series 10kV dry-type transformer is the standard reference for procurement. The Tianan online factory tour documents the resin casting line and PD test bay.
The 10-check audit below covers what EPC procurement teams should verify during the supplier qualification visit, with each point mapped to the failure mode that the audit catches.

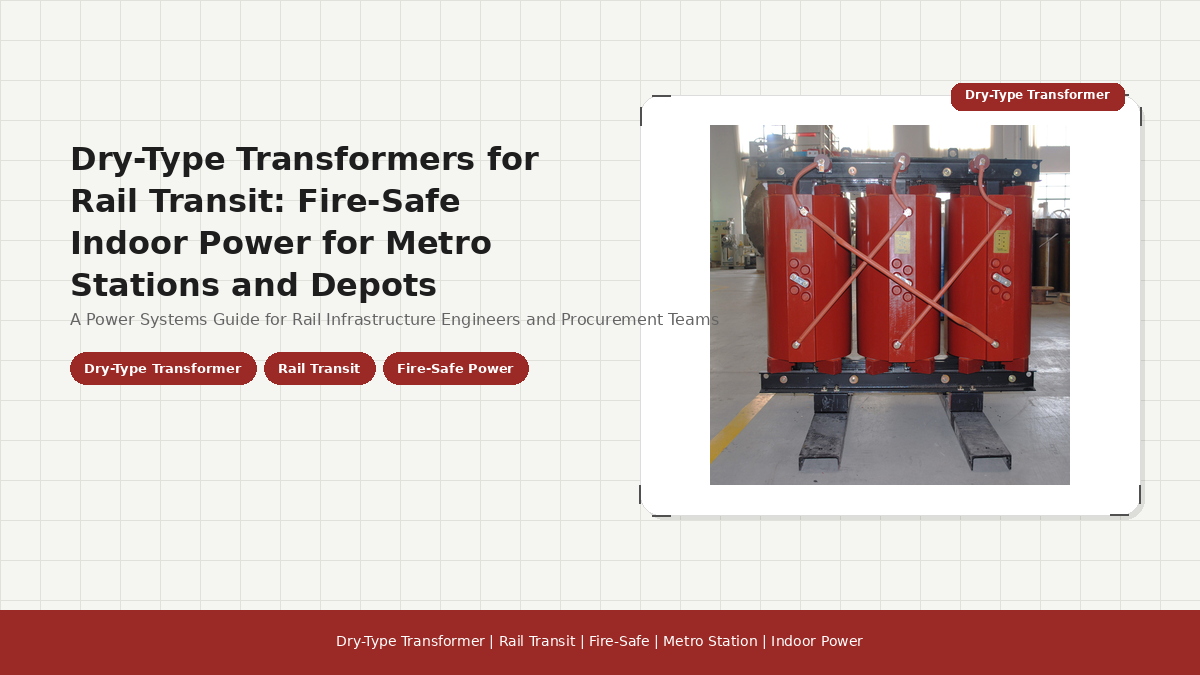
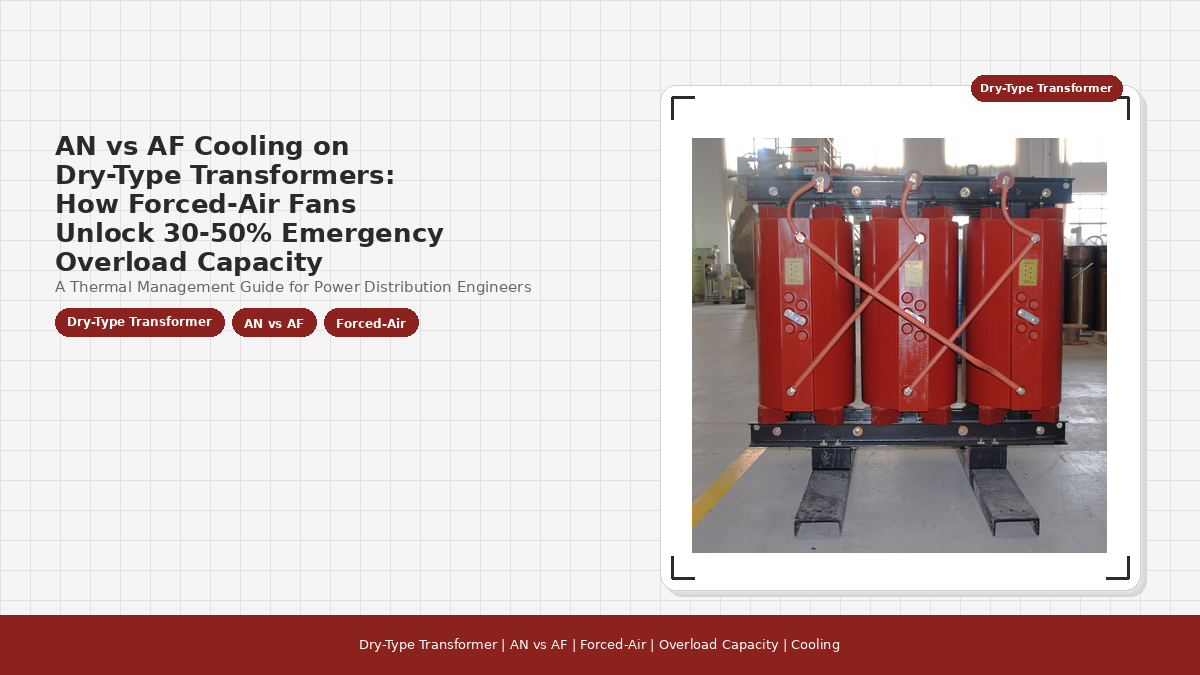
SC series 10kV cast-resin dry type transformer — the standard reference for indoor substation procurement. View product →
The Indoor Substation That Triggered a Fire Drill on Day 91
An EPC contractor in northern Europe contacted us in early 2025 after a dry type transformer they had sourced from a different Chinese supplier tripped the building fire alarm system on day 91 of operation. The transformer was installed in the basement of a hospital, and the partial discharge events had increased to the point where the smoke detection system triggered the building evacuation. Investigation revealed that the cast-resin insulation had voids that produced elevated partial discharge, which generated ozone and aerosol particles that triggered the smoke detector. The transformer was still electrically functional, but the indoor substation had to be taken offline for emergency replacement.
The structural cause was a manufacturing process issue at the supplier's vacuum casting line. The casting process had produced void defects in the high voltage coil insulation, which are the root cause of partial discharge events. The void defects were not detected at the supplier's factory because the supplier's PD test bay was not part of the standard production test routine. The void defects would have been detected by a 10-minute PD test that costs the supplier virtually nothing to perform.
The EPC contractor's fix was to require the supplier to provide PD test reports per IEC 60076-11 as part of the routine test documentation for every unit. The new agreement with Tianan covered the SC series dry type transformer with mandatory PD testing at the supplier's dedicated PD test bay. The new transformer has been in operation for 12+ months without partial discharge events, and the indoor substation has passed three quarterly fire safety inspections.
The structural insight: the PD test bay is the single most important stop on the factory tour. Programs that skip the PD test bay verification catch the manufacturing issue only after the transformer is installed. Indoor Transformer Installation fire safety requirements are documented through theNFPA fire safety standards.
Why Dry Type Matters for Indoor Substations (and the EPC Risk If It Fails)
Dry type transformers use solid insulation (epoxy resin or cast resin) instead of oil for the winding-to-winding and winding-to-ground insulation. The dry type construction eliminates flammable oil and the associated fire risk, making dry type the standard specification for indoor substations, building-integrated substations, hospitals, and data centers.
The risk profile for dry type transformer failures is structurally different from Oil-Immersed Transformer failures.Oil-immersed transformer failures typically result in oil leaks and potential fire escalation; dry type transformer failures typically result in partial discharge events that generate ozone and aerosol particles that can trigger fire detection systems. The dry type failure mode is less dramatic but more disruptive to the indoor installation, because the indoor substation has to be taken offline for replacement even when the transformer is still electrically functional.
For EPC procurement teams targeting indoor substation applications, the dry type transformer specification is the structural decision that determines the long-term reliability of the indoor substation. Programs that source dry type transformers based on catalog specifications without verifying the cast-resin quality and PD test bay encounter the failure mode that the audit prevents.
The IEC 60076-11 standard for dry type transformers specifies the partial discharge limits, the temperature rise limits, the short-circuit withstand requirements, and the type test protocols. Programs that require IEC 60076-11 compliance with current PD test reports receive dry type transformers that meet the indoor substation reliability requirements.
The 10-Check Factory Audit: Vacuum Casting, Windings, and PD Test Bays
The 10-check factory audit covers three categories: vacuum casting (4 checks), windings (3 checks), and PD test bay (3 checks). Each check is verified through documentation review, physical observation, and interview.
Category 1: Vacuum Casting (4 checks)
- Vacuum level verification. the vacuum casting chamber must achieve below 10 mbar vacuum level for the resin to flow into the coil without trapping air pockets. Verify the vacuum gauge calibration and the documented vacuum level achieved on the last 10 production coils.
- Resin mixing and degassing. the epoxy resin must be mixed and degassed under vacuum before the casting. Verify the resin mixing station and the documented degassing time.
- Curing temperature profile. the curing oven must achieve the documented temperature profile for the resin system. Verify the oven temperature recording and the documented cure time.
- Cast surface inspection. the cast coil surface must be inspected for cracks, voids, and contamination. Verify the inspection procedure and the recent inspection records.
Category 2: Windings (3 checks)
- Conductor material verification. the winding conductor must be the specified copper or aluminum material with the documented cross-section. Verify the conductor material certificates and the in-process conductor inspection.
- Winding tension and turn count. the winding tension and turn count must match the design specification. Verify the winding machine settings and the recent production records.
- Insulation paper application. the inter-layer insulation paper must be properly applied with the correct overlap and tension. Verify the paper material certificates and the application inspection records.
Category 3: PD Test Bay (3 checks)
- PD measurement equipment. the PD test bay must have calibrated PD measurement equipment capable of detecting PD below 10 pC at the rated voltage. Verify the equipment calibration records and the PD measurement procedure.
- PD test protocol. the supplier must perform the PD test on every production coil per IEC 60076-11. Verify the documented PD test report for recent production coils.
- PD failure handling. the supplier must have a documented procedure for handling coils that fail the PD test. Verify the re-work or scrap procedure and the recent PD failure records.
The 10-check format is designed for 1-2 days on-site, with each check verified by documentation review, physical observation, and interview. Findings are documented in a pass/conditional/fail format.
The Vacuum Casting Process: Where Most Quality Failures Start
The vacuum casting process encapsulates the high voltage winding in epoxy resin under vacuum conditions to produce void-free insulation. The process involves placing the wound coil in a mold, evacuating the air (typically to below 10 mbar), introducing the epoxy resin, and curing under controlled temperature. The vacuum is critical to remove air pockets that would otherwise create void defects where partial discharge events originate.
Most quality failures in cast-resin dry type transformers start at the vacuum casting process. The void defects from inadequate vacuum, contaminated resin, or improper curing temperature cause partial discharge events that eventually lead to insulation failure. The typical failure progression is:
- Initial void defects: from inadequate vacuum or contaminated resin, present at the time of casting.
- PD events begin: small electrical discharges within the void defects, typically measurable at the routine PD test if the test is performed.
- Progressive insulation degradation: PD events gradually erode the surrounding insulation, increasing the void size and the PD magnitude.
- Insulation failure: typically after years of service, the cumulative damage leads to a complete insulation breakdown.
The structural fix for the casting failure mode is the supplier's PD test at the end of the casting process. A well-cast high voltage coil typically has PD below 10 pC at rated voltage per IEC 60076-11. A poorly cast coil with voids or contamination shows elevated PD, which predicts premature insulation failure in service. The PD test is the single most important quality verification for cast-resin dry type transformers.
The structural prevention is the supplier's vacuum casting process control. The supplier should have documented vacuum level records, resin mixing records, and curing temperature records for every production coil. The audit verifies these records are consistent with IEC 60076-11 requirements.
PD Test Bay: The Single Most Important Stop on the Factory Tour
The PD test bay is the single most important stop on the factory tour for dry type transformer procurement. The PD test is the structural verification that the cast-resin quality meets the IEC 60076-11 requirements, and the supplier's PD test bay capability is the structural verification that the supplier can perform the PD test consistently across production.
Five items for the PD test bay visit:
- PD measurement equipment: confirm the supplier has calibrated PD measurement equipment capable of detecting PD below 10 pC at the rated voltage. The equipment should be from a recognized manufacturer (e.g., Omicron, Haefely, B2 HV) with current calibration certificates.
- PD test procedure: confirm the supplier has a documented PD test procedure that follows IEC 60076-11, with the test voltage, test duration, and acceptance criteria specified.
- Recent PD test reports: review the PD test reports for the last 10 production coils to verify the PD values are consistently below the acceptance criteria. The audit team should look for trends or occasional outliers that indicate process instability.
- PD failure handling: confirm the supplier has a documented procedure for handling coils that fail the PD test, including re-work or scrap decisions. The PD failure rate is a structural indicator of the casting process quality.
- PD test as standard routine test: confirm the supplier performs the PD test on every production unit as part of the standard routine test, not only on the type test units. The PD test is the most value when performed on every unit.
The [Tianan online factory tour](https://www.tiananoverseas.com/factory-tour/) documents the resin casting line and PD test bay. The PD test bay is positioned after casting and before final assembly, allowing the supplier to address PD failures before units are committed.
Class F vs Class H Insulation: What the Temperature Class Actually Means for Your Substation
The insulation temperature class determines the maximum operating temperature of the transformer winding and the temperature rise limit during the routine test. Class F insulation has a maximum operating temperature of 155°C, while Class H insulation has a maximum operating temperature of 180°C.
The temperature class selection affects the substation specification in three ways:
- Overload capacity. Class H insulation provides higher overload capacity (typically 20-30% above rated) for short-duration peak loads, while Class F provides standard overload capacity. Programs with high peak-to-average load ratios (data centers, hospitals) benefit from Class H overhead.
- Insulation life. the insulation life follows the Arrhenius equation, with each 10°C increase in operating temperature approximately halving the insulation life. Class F operating at 130°C (rated minus 25°C margin) provides approximately 30 years of insulation life, while Class H operating at 155°C provides approximately the same life with more overload headroom.
- Cost premium. Class H materials cost more than Class F materials. The cost premium is typically 10-20% on the unit price.
For indoor substation applications, Class F is the standard for most projects. Class H is specified for high-overload applications or elevated ambient temperature installations. The temperature class should be specified at the procurement stage based on the substation's expected load profile and ambient temperature.
Three Procurement Programs and What Their Audits Caught at the Test Bay
Three EPC procurement programs illustrate how the 10-check audit catches quality issues that the documentation audit misses.
Program 1: Hospital indoor substation, Northern Europe, 4 units. Original audit: documentation only. The 10-check audit caught that the supplier's PD test reports had not been issued for 6 months. The supplier re-tested all units; 2 had PD above the IEC 60076-11 limit. The supplier re-cast the 2 failing units. The corrected units passed the PD test, and the hospital inspection passed on the first review.
Program 2: Data center indoor substation, Southeast Asia, 6 units. Original audit: documentation only. The 10-check audit caught the supplier's vacuum casting chamber had a vacuum leak producing higher vacuum levels than documented. The leak was repaired and coils re-tested. PD values dropped by approximately 30% after the repair, confirming the leak as the root cause.
Program 3: Industrial plant substation, Middle East, 3 units. Original audit: documentation only. The 10-check audit caught the supplier's curing oven temperature was inconsistent across the production batch. Lesson: process verification catches the documentation issue that the audit would have missed.
The common thread across all three programs: the 10-check audit caught quality issues that documentation missed, and the corrective action prevented expensive field failures. Programs that include the audit consistently deliver reliable dry type transformers.
Sourcing Dry Type Transformers From Tianan Overseas
For EPC procurement teams sourcing dry type transformers, six items should be covered before the PO is released.
- Transformer specification: voltage class, capacity rating, vector group, impedance, and temperature class (F or H).
- Standard compliance: IEC 60076-11 with current type test report and PD test report per the supplier's design.
- Quality assurance documentation: factory audit report from the 10-check protocol, with PD test records from recent production coils.
- Factory acceptance test: witnessed FAT with PD test included in the routine test, plus temperature rise test for the temperature class verification.
- Delivery and installation: shipping packaging, transportation, on-site installation support, and commissioning documentation.
- Long-term support: warranty terms, spare parts availability, and PD testing support for the in-service verification.
The Tianan dry-type transformer manufacturing scope covers the SC series and resin casting lines, with the SC series 10kV dry-type transformer as the standard reference for indoor substation procurement. The Tianan online factory tour documents the 120,000 m² production base with the dedicated resin casting line and PD test bay.
For EPC procurement teams new to dry type sourcing, the 10-check audit is the first step in supplier qualification, taking 1-2 days on-site.
Request 10-Check Audit Schedule for Your Program
Tell us your project specification, voltage class, capacity rating, and temperature class. We will provide the 10-check audit protocol and FAT plan for your dry type transformer procurement program.
Request Audit Schedule →Frequently Asked Questions
What is a dry type transformer and why is it used for indoor substations?
A dry type transformer uses solid insulation (epoxy resin, cast resin) instead of oil for the winding-to-winding and winding-to-ground insulation. The dry type construction eliminates flammable oil and fire risk, making dry type the standard specification for indoor substations, building-integrated substations, hospitals, and data centers. The trade-off is reduced overload capacity and higher cost, but the safety benefit typically justifies the price premium for indoor applications.
What is IEC 60076-11 and why does it matter for dry type transformers?
IEC 60076-11 is the international standard for dry type power transformers, covering design, manufacturing, testing, and performance requirements. The IEC 60076-11 is published through the IEC. The standard is published by the International Electrotechnical Commission (IEC) and is the structural reference for dry type transformer specifications globally. The IEC 60076-11 standard specifies the partial discharge limits, the temperature rise limits, the short-circuit withstand requirements, and the type test protocols. The supplier's type test report per IEC 60076-11 is the structural verification that the dry type transformer design meets the international standard. Reference standards are published through the IEEE Power & Energy Society.
What is the partial discharge test for dry type transformers?
The partial discharge (PD) test measures small electrical discharges within the insulation system under high voltage stress. For dry type transformers, the PD test verifies that the vacuum casting process produced void-free insulation. A well-cast coil has PD below 10 pC at rated voltage per IEC 60076-11. A poorly cast coil shows elevated PD, predicting premature failure. The PD test is the single most important quality verification.
What is the difference between Class F and Class H insulation for dry type transformers?
Class F has a maximum operating temperature of 155°C; Class H has 180°C. The temperature class determines overload capacity and long-term insulation life. Class F is standard for most indoor applications; Class H for higher overload or higher ambient temperature.
What is the vacuum casting process for dry type transformers?
The vacuum casting process encapsulates the high voltage winding in epoxy resin under vacuum (typically below 10 mbar) to produce void-free insulation. The vacuum is critical to remove air pockets that create void defects. This is the most quality-sensitive step in cast-resin dry type manufacturing.
How long does a dry type transformer last?
Cast-resin dry type transformers typically have a service life of 25-30 years with proper maintenance. The insulation life is determined by the operating temperature and the number of thermal cycles during the service life. Class F insulation operating at 80% of rated temperature provides approximately 30 years of service life, while Class H insulation operating at the same temperature provides longer service life. The dry type transformer life is also determined by the partial discharge performance, with low-PD castings showing longer insulation life than high-PD castings.
What is the noise level of a dry type transformer?
Cast-resin dry type transformers typically operate at lower noise levels than oil-immersed transformers of equivalent rating, with typical noise levels of 50-60 dB(A) at 1 meter distance. The lower noise is because the dry type construction eliminates oil cooling system noise. For indoor substation applications where noise is a concern, the dry type noise level is typically within building acoustic requirement without sound attenuation.
What is the minimum order quantity for dry type transformers from a Chinese supplier?
Typical MOQ for dry type transformers from a Chinese supplier is 1-3 units for the initial production run, depending on rating and supplier capacity. The MOQ is typically lower than for oil-immersed transformers because the dry type production line is more flexible. EPC programs should confirm MOQ at the supplier qualification stage with delivery time specification.