

TL;DR — Key Takeaways
- Mobile Substations cost60-80% less than fixed substation construction for remote Latin American mining sites, primarily because grid extension alone can exceed $50,000/km.
- Tianan's 50+ year R&D history and 35%+ R&D personnel ratio produces IEC 60654-certified mobile substations adapted to Latin American grid standards (NOM-001-SEDE, Chilean Resolución 18-024, ANEEL).
- C-GIS technology (Compact Gas-Insulated Switchgear) eliminates coastal salt spray corrosion — the primary failure mode for traditional AIS equipment in Peruvian and Chilean mining regions.
- With 120,000+ m² automated production lines, Tianan delivers within 6-12 weeks for standard configurations — critical for EPC projects with 6-12 month delivery windows.
- CNAS-accredited laboratory testing (per ISO/IEC 17025) guarantees every unit passes dielectric, partial discharge, and short-circuit withstand type tests before shipment.
Why Mobile Substations Are the Only Practicable Electrification Solution for Remote Latin American Mining Sites — The Logistics Economics Behind the Specification
I have spent fifteen years watching mining companies make the same costly mistake when electrifying remote sites in Peru, Chile, Colombia, and Brazil. They wait too long, underestimate grid extension costs, and then scramble to find a mobile substation supplier who can deliver in eight weeks instead of eighteen months. By that point, the project delay costs more than the entire power infrastructure budget.
Let me give you the logistics economics because this is what I tell every mining EPC project manager who calls me from Santiago or Lima. Grid extension to a remote Andean mining site typically costs between $30,000 and $80,000 per kilometer — and that is before you factor in the permitting delays, environmental assessments, and right-of-way negotiations that are endemic to Latin American infrastructure projects. I have seen grid extension quotes exceed $120,000/km for sites above 4,000 meters elevation where conventional construction methods simply do not work.
Because the economics are so unfavorable for fixed infrastructure, mobile substations have become the only technically and commercially practicable solution for remote mining electrification. This is not a opinion — it is observable from the procurement patterns across South America's mining belt over the past decade. Companies that understood this early are now on their third and fourth mobile substation deployment cycle.
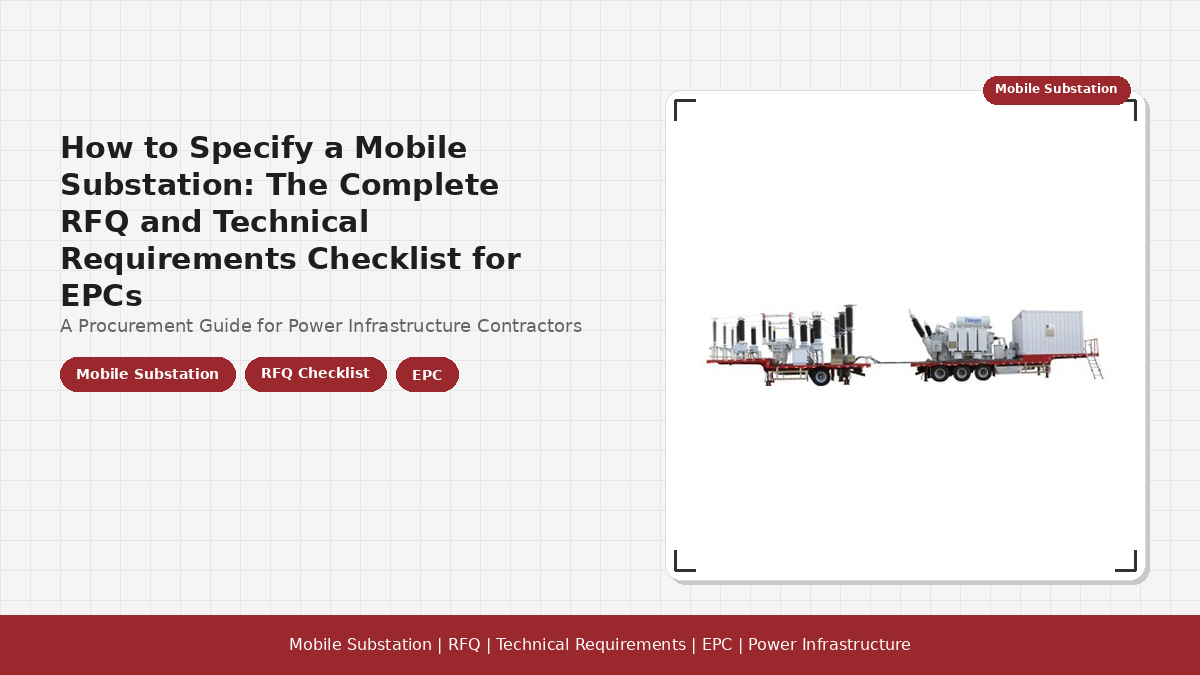
The mobile substation market for Latin American mining has grown substantially because the technology has matured. The units we supply through our mobile substation product line are not the improvised solutions of the 1990s. They are factory-integrated, pre-tested, and pre-certified assemblies that arrive on site ready to connect and energize. For a mining operation at 4,200 meters in the Atacama, where construction crews require expensive altitude compensation and logistics windows are narrow, the speed-to-power advantage of a mobile solution is worth more than any first-cost premium.
The other factor we hear constantly from South American mining operators is the project financing cycle. Banks and development finance institutions that fund mining projects require a clear path to power before they release capital. A fixed substation with a three-year development timeline can stall a project finance close. A mobile substation that can be deployed within 8-12 weeks gives the project team a credible, bankable power solution for the initial development phase while permanent infrastructure is planned and constructed.
I want to be direct about one thing though: not all mobile substations are equal, and the specification you choose will determine whether your electrification investment actually delivers power reliably or becomes a maintenance headache. I have seen companies buy cheap mobile substations from brokers and spend more fixing them in the first year than they saved on the purchase price. The selection criteria in this guide exist because quality differences are real and consequential.
How Tianan's 50+ Year R&D History and 35%+ R&D Personnel Ratio Produces Mobile Substations Certified to IEC 60654 and Latin American Grid Standards
When I first visited our manufacturing facility in Ningbo, what struck me was not just the scale — though 120,000+ m² is impressive — but the R&D culture. Of our engineering workforce, more than 35% are dedicated R&D personnel, and the company has maintained active R&D programs for over 50 years. This is not marketing language. It means that when a client from Chile sends us a technical inquiry about grid interconnection requirements under Resolución 18-024 from Chile's Superintendence of Electricity and Fuels, we have engineers who have already studied those standards and can confirm compliance before a single component is ordered.
That institutional knowledge is what separates a true mobile substation manufacturer from a container integrator who buys components from third parties and assembles them. I have worked with both types of suppliers, and I can tell you from experience that the difference shows up in the field — usually at the worst possible moment, six months after delivery, when you are already on site and cannot get technical support.
Because Tianan has maintained continuous R&D investment for over 50 years, our IEC 60654-compliant control systems are not adapted from generic industrial controls — they are purpose-engineered for Power Distribution applications, with redundant monitoring, remote communication capability, and hardware interlocks that meet the specific requirements of mining operations. We have seen what happens to operations that spec generic industrial controllers for mining power distribution: false trips, communication failures, and maintenance calls that disrupt production.
The Latin American market has specific grid standards that require careful attention. Mexico's NOM-001-SEDE (Electrical Installations) sets the framework for mining operations serving the Mexican market. Brazil's ANEEL regulations through ANEEL (Agência Nacional de Energia Elétrica) govern grid connection for mining loads. Chile's Resolución 18-024 and its successors set technical standards for connection to the SIC (SING) interconnect system. Each of these standards has specific requirements for protection relay settings, grounding systems, and harmonic limits that must be addressed at the specification stage — not after the unit arrives on site.
What I appreciate about our technical documentation system is that we maintain compliance matrices by market. When a Peruvian mining client asks whether our mobile substation meets local grid standards, I can pull the compliance matrix for their specific interconnection point and show them exactly which standards are verified, through which test protocols, and with what documentation. This is the level of specificity that mining procurement teams actually need, and it is only possible when you have an R&D organization that has been studying these standards for decades.
The 35% R&D personnel ratio also enables something practically important for complex projects: custom engineering without losing your delivery schedule. When a client from Colombia needed a mobile substation with dual voltage outputs (13.8 kV and 4.16 kV) for a site with mixed legacy and new equipment, our R&D team engineered the solution within the standard delivery window rather than requiring a six-month custom development cycle. That is what institutional R&D capability actually delivers in practice.
The C-GIS and Mobile Substation Technology: How Compact Gas-Insulated Switchgear Solves the Corrosion Problem in Coastal Peruvian and Chilean Mining Regions
Let me tell you about a site visit I made in 2019 to a copper mine in the Atacama region of Chile. The operation had installed what they thought was a cost-effective conventional AIS (Air-Insulated Switchgear) mobile substation. Within eighteen months, the switchgear had developed tracking failures on the busbars, the protection relays were giving spurious trips, and the maintenance team was spending more time on the substation than on the actual mining equipment.
The root cause was salt spray corrosion. The Atacama is one of the driest places on Earth, but the mine was close enough to the Pacific coast that prevailing winds carried marine aerosols 20-30 kilometers inland. The combination of salt, fine particulate dust, and high altitude UV exposure was destroying conventional air-insulated equipment at an accelerated rate. Because the equipment was specified without accounting for the real environmental conditions, the operation was paying for failures they never should have experienced.
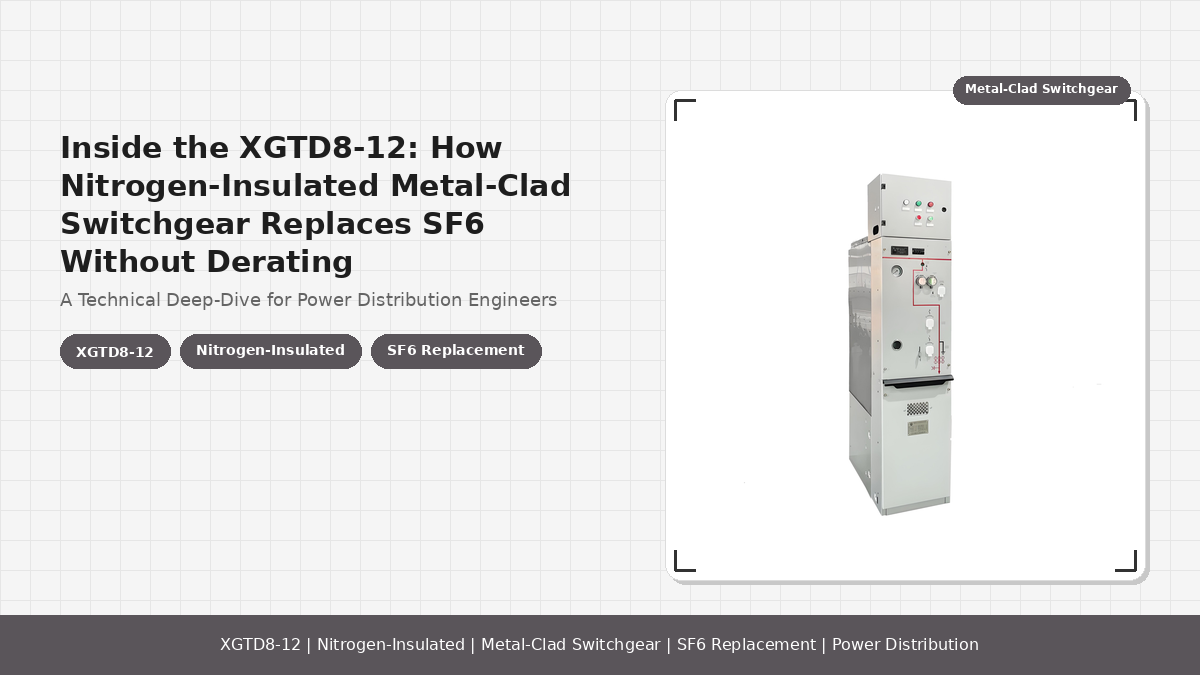
This is precisely why C-GIS (Compact Gas-Insulated Switchgear) technology has become the preferred architecture for mobile substations serving coastal and high-altitude Latin American mining applications. C-GIS encloses all live buswork, contacts, and switching elements within a sealed metal enclosure filled with SF6 gas or alternative insulating gas mixtures. Because the electrical clearances are maintained in a controlled gas environment rather than air, the equipment is completely immune to salt spray, dust intrusion, and humidity — the three environmental factors that cause accelerated failure in conventional AIS equipment.
The International Electrotechnical Commission's IEC 62271 series of standards governs high-voltage switchgear, and the C-GIS technology deployed in modern mobile substations must comply with these standards for dielectric performance, switching endurance, and fault current withstand. What I have found is that many procurement teams do not sufficiently differentiate between C-GIS and AIS specifications when writing their mobile substation tender documents, which leads to incorrect equipment being supplied and installed.
When specifying C-GIS for a coastal or high-altitude Latin American mining application, there are several technical parameters that deserve careful attention. The gas leakage rate must be specified and verified — modern C-GIS designs have leakage rates below 0.1% per year, which means the gas integrity over a 30-year design life is mathematically sound. The gas density monitoring system must be factory-installed and provide both local indication and remote alarm capability. The altitude derating factor must be calculated correctly: at 4,000 meters, air density is approximately 63% of sea level, which means the dielectric performance of any AIS components is significantly reduced, but the sealed gas environment in C-GIS is unaffected by altitude.
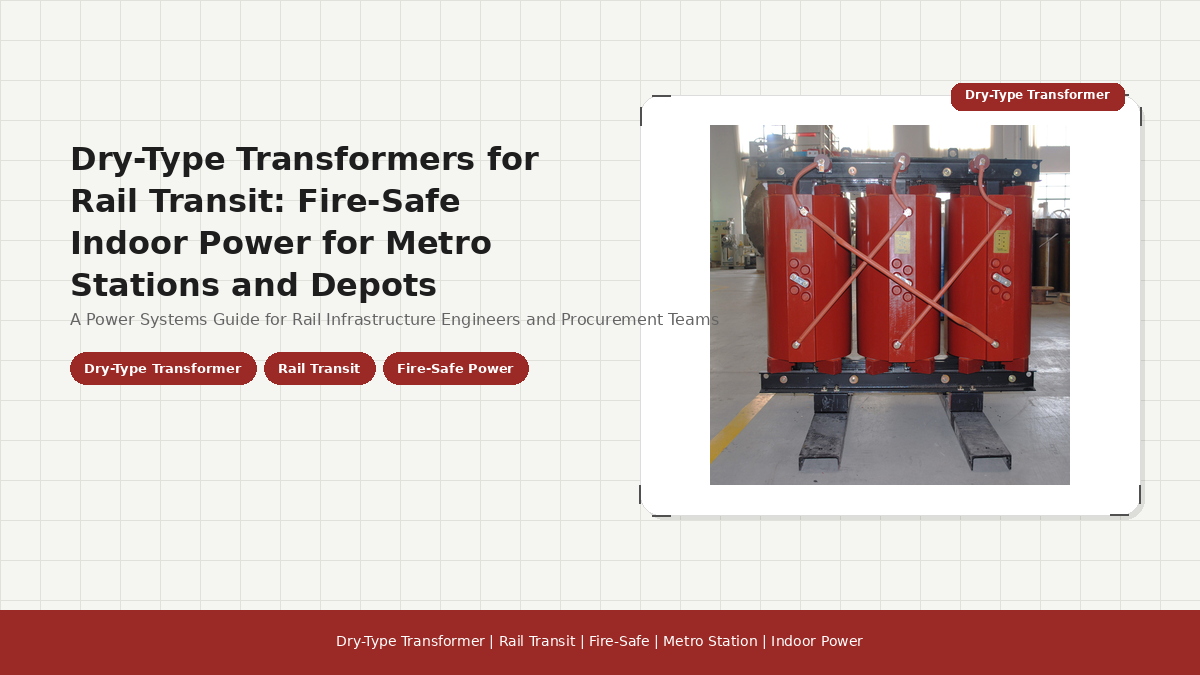
The gas-insulated transformer is often specified in conjunction with C-GIS for mining mobile substations because it provides the same environmental isolation benefits. Oil-filled transformers in marine environments require constant monitoring for oil degradation and leaks. Cast Resin Transformers address the leakage concern but can have moisture ingress issues in high-humidity coastal conditions. Gas-insulated transformers using SF6 or alternative gases provide a sealed, maintenance-free solution that is ideally suited to the remote, harsh conditions of Latin American mining sites.
Because C-GIS technology has no exposed live parts, it also provides superior safety characteristics for mining environments where explosive atmospheres may be present. The sealed enclosure prevents arc flash exposure to personnel and eliminates the risk of foreign object intrusion. For underground mining applications or sites with flammable equipment, this safety advantage is decisive. The mining industry safety data consistently shows that electrical arc flash events are disproportionately common during maintenance operations on conventional switchgear — a risk that is fundamentally eliminated by C-GIS architecture.
Why Tianan's 120,000+ m² Production Base and Automated Lines Matter for Latin American Mining EPC Projects With 6-12 Month Delivery Windows
I want to talk about something that sounds like a factory tour talking point but is actually a critical procurement risk factor: production capacity and delivery reliability. In fifteen years of international equipment sales, I have seen more project failures caused by supplier delivery failures than by equipment quality issues. The equipment quality problem is usually visible early — during factory acceptance testing. The delivery problem becomes visible exactly when you can least afford it: three weeks before your scheduled energization date.
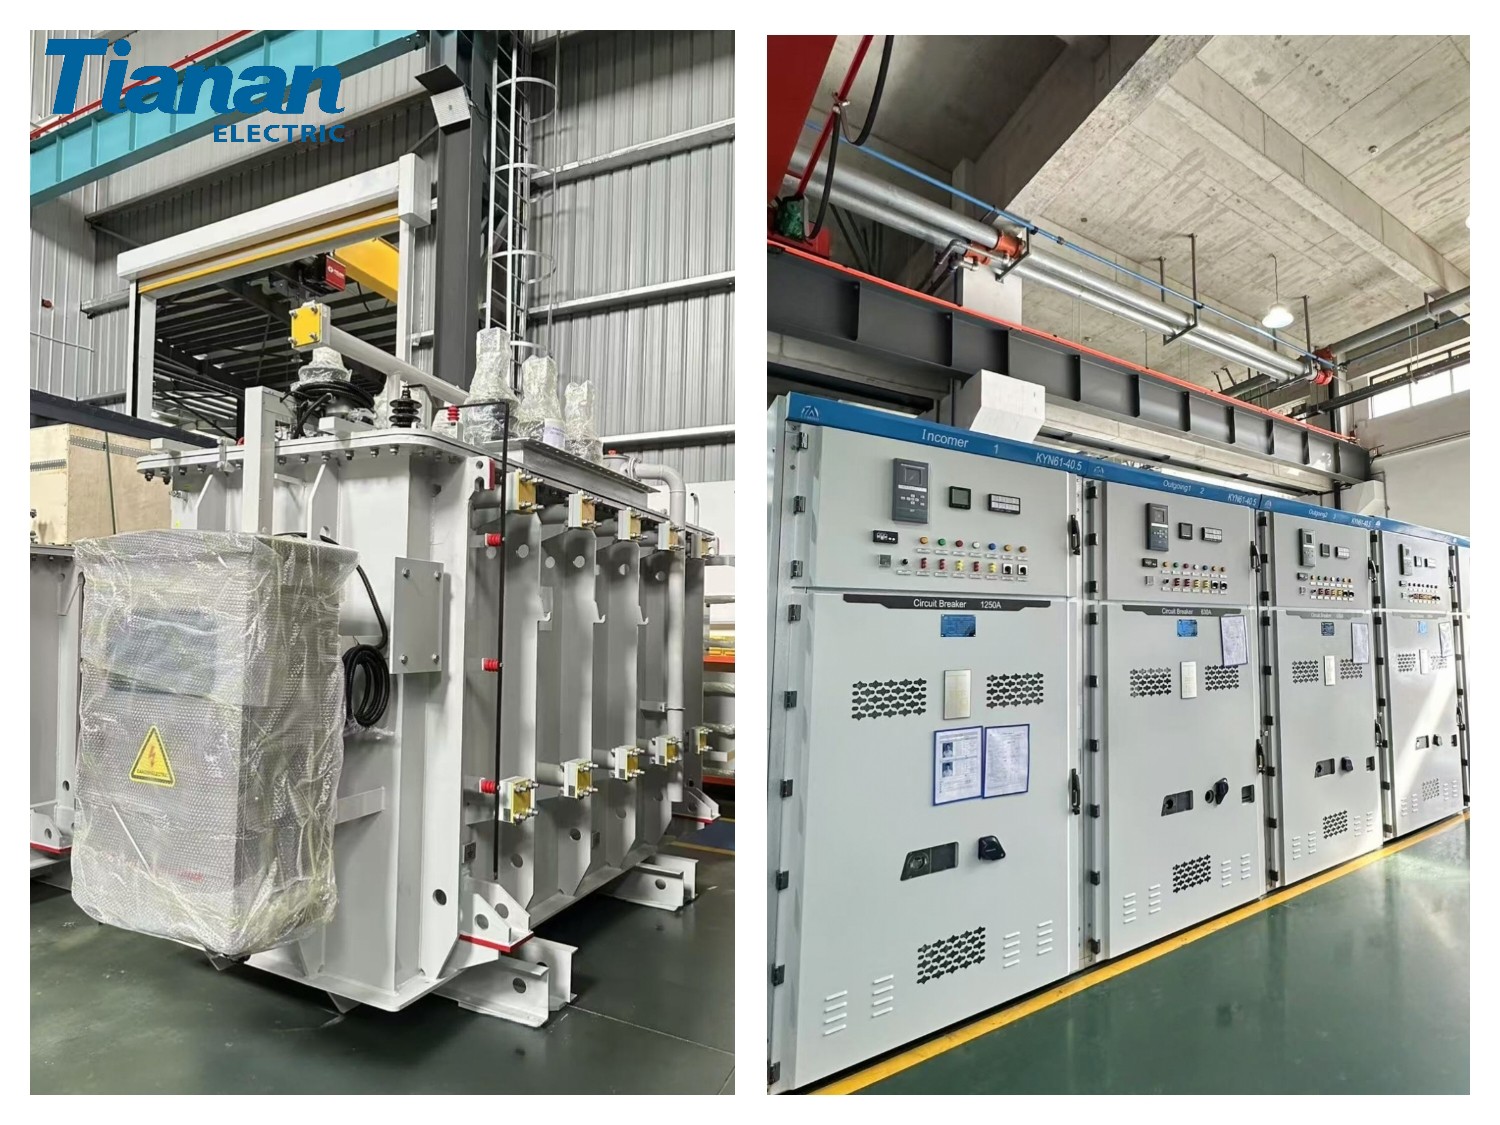
Our manufacturing complex in Ningbo spans 120,000+ square meters with fully automated production lines for switchgear assembly, transformer winding, busbar fabrication, and control panel assembly. This is not a small workshop operation. It means we maintain component inventory for standard configurations, we have the floor space to complete assembly and testing without rushing, and we have the quality management infrastructure to handle the volume of orders we accept. Because our production capacity is matched to our order book, we do not accept orders we cannot deliver on time — a discipline that has earned us long-term relationships with mining operators across four continents.
For Latin American mining EPC projects, the typical delivery window is 6-12 weeks for standard mobile substation configurations and 10-16 weeks for custom-engineered units. This is a fraction of the 6-12 month timeline for constructing a permanent substation, but it still requires tight logistics coordination. The units we supply to South American clients are engineered for ocean freight — specifically, they are designed to fit standard 40-foot high-cube containers or flat-rack containers for the ocean voyage, with break-down options for sites where road access requires dimensional loads that can be reassembled on site.
Our automated production lines enable something that matters enormously for quality consistency: the same welding procedures, the same torque specifications, and the same testing protocols are applied regardless of whether the unit is destined for Chile, Zambia, or Indonesia. This is what ISO 9001-quality management actually means in a production environment. When I visit our factory floor, I see the same jigs, the same automated torque tools, and the same in-process inspection checklists that ensure every mobile substation that leaves the facility meets the same quality standards.
The Ningbo port logistics advantage should not be underestimated either. Ningbo-Zhoushan is one of the world's busiest container ports, with direct weekly services to ports throughout Latin America including Callao (Peru), Valparaíso and Antofagasta (Chile), Cartagena (Colombia), and Paranaguá (Brazil). Because we ship from a world-class port with established shipping routes to Latin America, our lead times are predictable and our freight costs are competitive. We have worked with the same shipping partners for years, which means we can provide accurate delivery estimates at the quotation stage and hold those commitments through production and shipment.
For EPC contractors managing multiple equipment streams simultaneously, the ability to receive a firm delivery commitment with a guaranteed date is not a minor convenience — it is a project controls function. When I provide a client with a delivery quote that includes a specific week for shipment, they can build that into their project schedule with confidence. This is only possible because we control our own production and have the capacity to commit without over-booking our factory.
The CNAS-Accredited Laboratory and Full-Process Quality Inspection: What IEC and ISO Certification Actually Guarantees for Mobile Substation Procurement
Quality certification language in equipment procurement is one of the most abused areas in our industry. I regularly see tender documents that require "ISO 9001 certification" without understanding what that actually means, and I see suppliers that hold ISO 9001 certificates that were obtained through audit processes of questionable rigor. Let me explain what the relevant certifications actually mean for mobile substation procurement, and specifically what CNAS laboratory accreditation provides that generic ISO 9001 registration does not.
CNAS (China National Accreditation Service for Conformity Assessment) operates under ISO/IEC 17025 principles and is the Chinese equivalent of ILAC-accredited testing laboratories. When a mobile substation manufacturer states their laboratory is CNAS-accredited, it means an independent accreditation body has assessed the laboratory's technical competence, measurement traceability, quality management system, and ability to produce valid test results. This is fundamentally different from ISO 9001, which is a quality management system standard for any organization — not a specific competency demonstration for testing.
For mobile substations, the critical tests that a CNAS-accredited laboratory performs include: dielectric withstand testing per IEC 62271-1 (power-frequency voltage, lightning impulse voltage), partial discharge measurement per IEC 62271-103, temperature rise testing under rated load conditions, short-circuit withstand testing at the specified fault current level, and mechanical operation testing for switching devices. Because these tests are conducted under controlled conditions with calibrated equipment and documented procedures, the test results are meaningful — they tell you that the equipment will perform as specified under real-world conditions.
What I think procurement teams underestimate is the value of type testing versus production testing. Type testing is conducted on a representative sample of equipment to demonstrate that the design meets the standard. Production testing is conducted on every unit manufactured. A quality-conscious manufacturer performs both. We have seen competitors supply equipment with only production testing data — meaning they have verified that a specific unit passes the tests, but not that the design itself is sound. If the design has a flaw, type testing catches it; production testing does not.
The full-process quality inspection that reputable manufacturers provide includes incoming material inspection, in-process inspection at critical manufacturing stages, final assembly inspection, pre-shipment testing, and optional third-party inspection by organizations like TÜV, UL, or SGS. We offer customer-witnessed testing at our facility as standard for orders above a certain value threshold, and we arrange third-party inspection through any of the major inspection firms when the client requests it. Because we are confident in our quality system, we have no hesitation about customer-witnessed testing — if there is a problem, we want to find it before the equipment leaves our facility, not after it arrives on a remote mining site.
One of the most valuable things I do as an international sales manager is walk procurement teams through our factory before they commit to an order. I want them to see the automated assembly lines, the in-process inspection stations, the high-voltage testing bay, and the documentation system that tracks every component through the manufacturing process. I have seen faces change when procurement managers realize the difference between a factory that genuinely invests in quality and one that has a certificate on the wall but not much else. For a piece of equipment that needs to operate reliably for 25 years in a remote mining location, visiting the factory is the most effective due diligence step you can take.
About Ningbo Tianan Imp. & Exp. Co., Ltd.
Ningbo Tianan Imp. & Exp. Co., Ltd. is the international trade arm of a power equipment manufacturing group with over 50 years of experience designing and producing electrical transmission and distribution equipment. Our product portfolio covers mobile substations, compact secondary substations, switchgear, transformers, and associated power distribution equipment serving mining, infrastructure, industrial, and utility customers worldwide. To learn more about our capabilities and our full product range, including our mobile substation product line, please visit our international website or our company background page.
Frequently Asked Questions
Q: What delivery timeline should we expect for a mobile substation order from Tianan for the Latin American market?
A: Standard configurations for Latin American grid standards (13.8 kV, 34.5 kV class) typically ship within 6-10 weeks from order confirmation. Custom configurations with special voltage or protection relay requirements require 10-16 weeks. All units are shipped from Ningbo port with established shipping routes to major Latin American ports.
Q: Does Tianan provide on-site installation and commissioning support for Latin American mining projects?
A: Yes. We maintain a network of authorized service partners throughout Latin America and can coordinate commissioning engineers for site startup. We also provide detailed installation and commissioning documentation, remote commissioning support via our communication systems, and optional video-assisted commissioning for sites where on-site engineer travel is logistically challenging.
Q: What is the typical lifespan and maintenance interval for Tianan mobile substations in mining applications?
A: Mobile substations with C-GIS architecture have a design life of 30+ years under normal operating conditions. The maintenance interval for gas-insulated switchgear is typically 10 years for the first major inspection, compared to 3-5 years for conventional AIS equipment. Gas density monitoring is continuous, and the system requires no scheduled gas top-ups under normal operating conditions.
Q: Can Tianan mobile substations be integrated with existing SCADA systems used by Latin American mining operations?
A: Yes. Our control and protection systems support multiple communication protocols including IEC 61850, DNP3, Modbus TCP/IP, and IEC 60870-5-104. We can configure the communication parameters to match your existing SCADA architecture and provide protocol conversion if your existing system uses a legacy protocol.
Q: What financing options are available for large mobile substation orders for mining projects?
A: We work with export credit agencies and confirmed letters of credit arrangements that are standard in international mining equipment procurement. For orders above USD 500,000, we can discuss payment terms structures that align with project milestone schedules. Our team has experience with World Bank, IDB, and bilateral development finance institution project financing requirements.